
ENGINEERED HEAVY-DUTY CONVEYOR SOLUTIONS
Chain Conveyors
Robust chain conveyor systems designed for reliable transport of pallets and heavy loads — engineered around your load requirements and material flow.
Overview
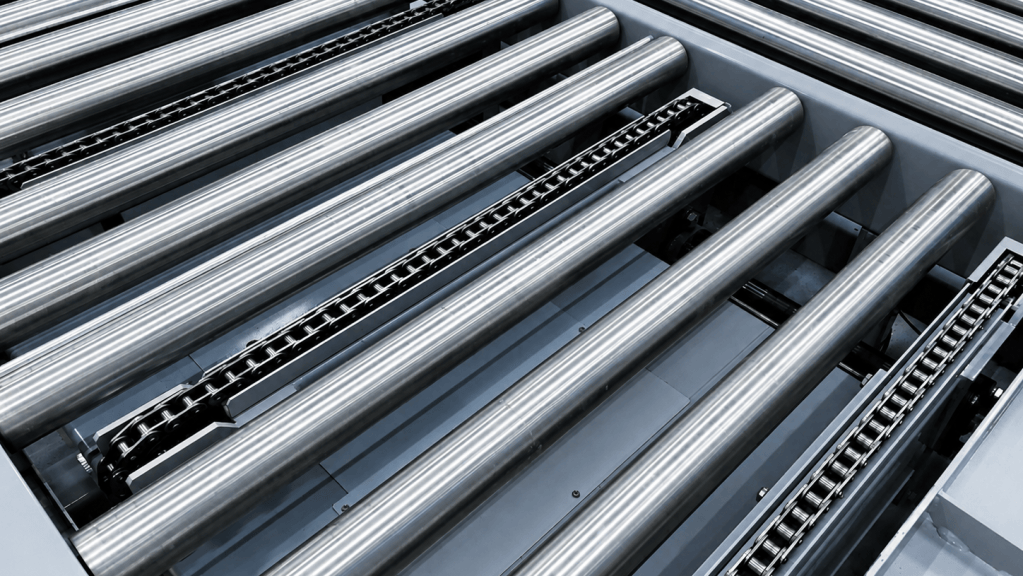
Chain conveyors use driven chain strands to transport pallets, containers and other heavy unit loads reliably between process areas. Each system is engineered according to load dimensions, weight, transfer requirements and operating conditions.
Key Features
- Heavy-duty material transport
- Suitable for pallets and heavy loads
- Robust industrial construction
- Configurable chain spacing
- Configurable conveyor lengths and speeds
- Reliable controlled load movement
- Integration with other conveyor systems
- Engineered around load and process requirements
Applications
Ideal for manufacturing plants, warehouses and logistics operations requiring reliable transport of pallets and heavy unit loads. Common applications include pallet transfer, production lines, buffer areas, assembly processes and automated material handling.
Optional Configurations
Chain conveyors can be configured with different numbers of chain strands, chain spacing, conveyor widths, lengths and speeds according to the application. Optional solutions include guides, stops, sensors, supports, safety guards and transfer interfaces with roller conveyors or other equipment.
Ready to Move Heavy Loads Reliably?
Get in touch with our team for a chain conveyor solution engineered around your loads and operation.